Good Manufacturing Practice (GMP) compliant manufacturing means producing drug products under GMP controls that meet regulatory expectations for quality, safety and consistency. Clinical manufacturing produces investigational materials for use in clinical trials (CTM), while commercial manufacturing produces drug products for market supply. Our facility supports both, with manufacturing controls, documentation and oversight aligned to MHRA, FDA and GMP requirements.
Moving a drug product from early-phase development through commercial supply requires manufacturing capability that scales with the program – without compromising compliance, quality or continuity. Disconnects between clinical and commercial manufacturing introduce risk during scale-up, technology transfer and regulatory progression, with the potential to delay clinical milestones and commercial launch.
We provide flexible, GMP-compliant clinical and commercial manufacturing services designed to support the full drug development lifecycle. Our MHRA and FDA-approved facility enables us to manufacture clinical trial materials and scalable commercial drug products, helping you transition efficiently from first-in-human and early-phase development through Phase III clinical supply and commercial manufacture. With advanced processing technologies, multiple GMP suites and experienced technical teams, we deliver quality, compliance and reliability at every stage.
Manufacture with confidence across the development life cycle
- Move seamlessly from clinical to commercial supplyIntegrated capability across the development lifecycle helps minimize risk during scale-up and supports efficient progression from early-phase studies to commercial manufacture.
- Manufacture under approved regulatory oversightOur MHRA and FDA-approved facility supports compliant clinical and commercial supply across major regulated markets.
- Access flexible batch sizesManufacturing capability is structured to support both clinical and commercial volumes, with flexibility aligned to program requirements.
- Apply advanced processing technologiesA broad range of processing capabilities – from blending and granulation through coating and lyophilization – supports diverse dosage forms and complex formulations.
- Work with experienced technical teamsSpecialist manufacturing expertise across dosage forms and processing technologies supports quality, compliance and reliability at every stage.
Our manufacturing capabilities
GMP manufacturing facility
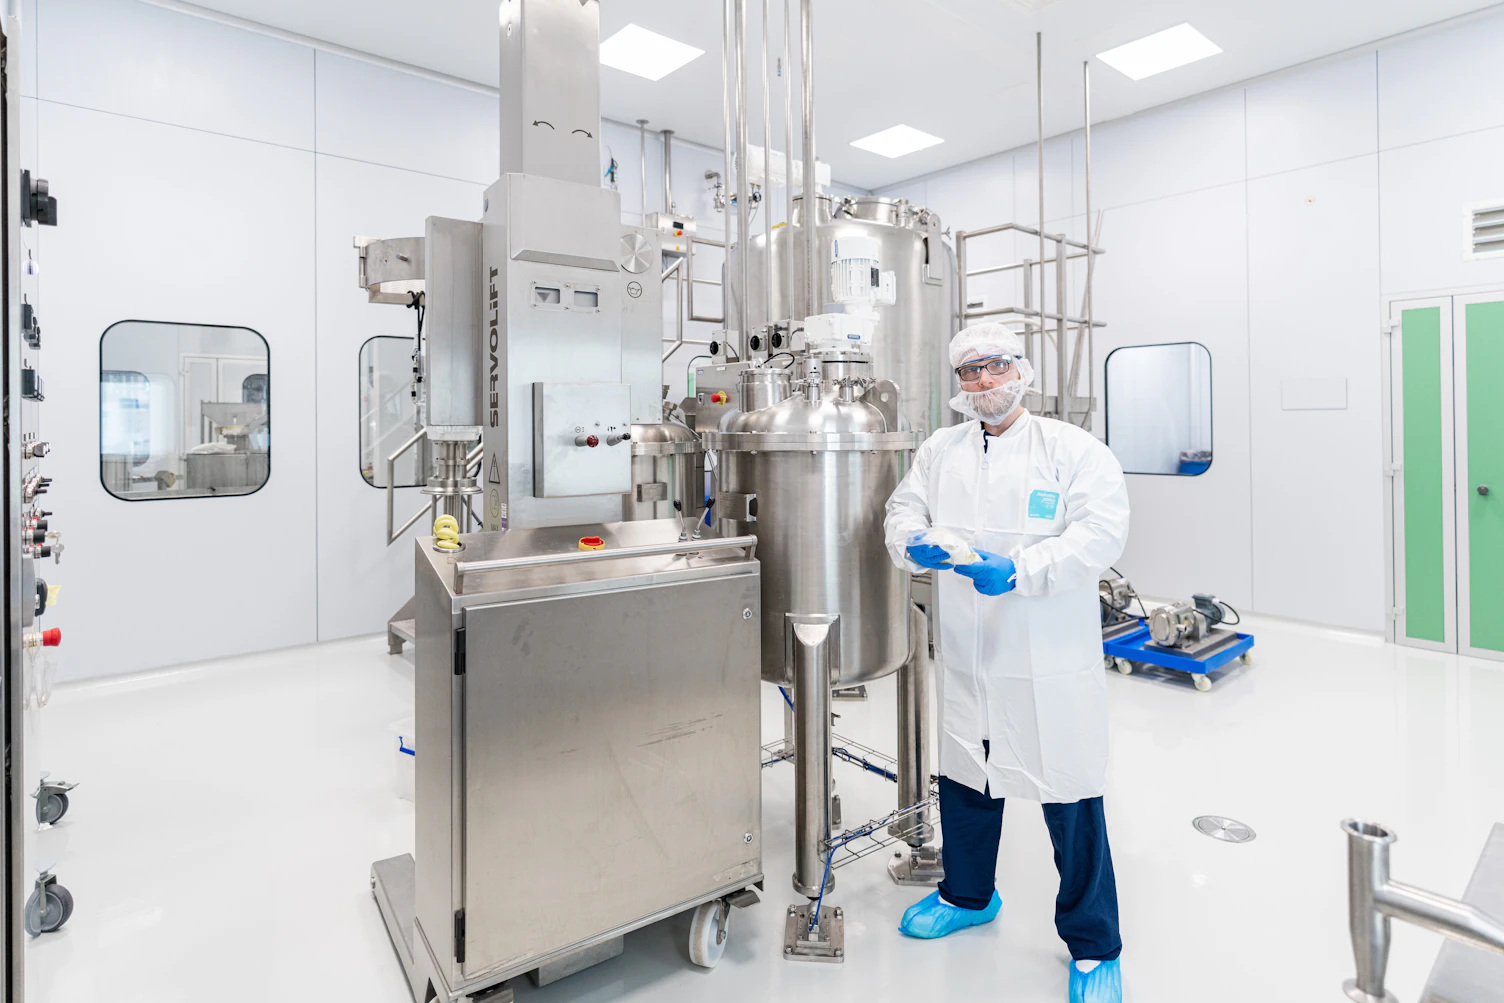
We operate an MHRA, FDA and GMP-approved 25,000 sq ft manufacturing facility with seven GMP manufacturing suites, supporting cGMP clinical trial material (CTM) production and flexible batch sizes for both clinical and commercial supply.
Dosage form capabilities
We manufacture across a broad range of dosage forms, including oral liquid solutions and suspensions, solid oral dose forms (powders, tablets and capsules), topical creams and ointments, and liquid-filled formats.
Core processing technologies
Our processing capabilities include blending, wet and dry granulation, direct compression for tablets and mini-tablets, encapsulation of powders, liquids, semi-solids and pellets, extrusion and spheronization, modified and aesthetic coating for tablets, capsules and pellets, capsule banding, and lyophilization.

Why SGS?
As the world's leading testing, inspection and certification company, we deliver clinical and commercial manufacturing from a single MHRA and FDA-approved facility, supported by integrated formulation development, analytical testing, packaging and CMC capabilities. This integration helps minimize risk during scale-up, supports continuity from early-phase development through commercial supply and provides the regulatory awareness needed to operate across major markets.
With multiple GMP suites, advanced processing technologies and experienced technical teams, we deliver the quality, compliance and reliability required to support programs from first-in-human studies through commercial manufacture.
FAQs
Yes. Our manufacturing facility is approved by the UK Medicines and Healthcare products Regulatory Agency (MHRA) and the US Food and Drug Administration (FDA), and operates under GMP. This approval supports clinical and commercial supply across major regulated markets.
We operate a 25,000 sq ft facility with seven GMP manufacturing suites, supporting flexible batch sizes for both clinical and commercial supply. This capability supports the full development life cycle – from first-in-human and early-phase studies through Phase III clinical supply and commercial manufacture.
Our manufacturing capabilities cover a broad range of dosage forms, including oral liquid solutions and suspensions, solid oral dose forms (powders, tablets and capsules), topical creams and ointments, and liquid-filled formats.
Our core processing technologies include blending, wet and dry granulation, direct compression (for tablets and mini tablets), encapsulation (powders, liquids, semi-solids and pellets), extrusion and spheronization, coating (modified or aesthetic – for tablets, capsules and pellets), capsule banding and lyophilization.
Yes. Our integrated capability supports efficient progression from clinical to commercial supply within a single facility, helping minimize risk during scale-up and technology transfer. This continuity is supported by alignment with our formulation development, analytical testing, CMC and packaging capabilities across our Contract Development and Manufacturing Organization (CDMO) portfolio.
Yes. We produce cGMP clinical trial materials across a range of dosage forms, supporting first-in-human studies, early-phase development and Phase III clinical supply. Clinical trial material production operates within the same approved facility as commercial manufacture, supporting consistency and continuity across the program life cycle.
Our clinical and commercial manufacturing is integrated with our formulation development, analytical testing, CMC and regulatory support, and packaging, labeling and distribution capabilities. This integration provides program continuity, reduces handoff risk and supports a coordinated approach to quality and compliance from early development through commercial supply.

Quay House, 28 Parkway Deeside Ind. Park,
CH5 2NS,
Flintshire, Wales, United Kingdom